 English
 Česká republika
 Deutsch
 Dutch
 Polska
How to Choose Food Grade Laminating Adhesive?
Choosing a Food Grade Laminating Adhesive is not simply a matter of selecting a product labeled “food safe.” The adhesive must suit the packaging structure, filling process, and expected storage conditions. A pouch holding oily snacks faces different demands from a retort pack exposed to heat and pressure. Small details matter.
Smithers’ report, The Future of Global Packaging to 2028, forecasts that the global packaging market will reach approximately $1.2 trillion by 2028. That scale reflects growing demands on packaging performance, consistency, and material efficiency. For converters, adhesive selection affects bond strength, production speed, and the risk of unwanted substance transfer. FDA 21 CFR 175.105 addresses adhesives used in food packaging, but applicability depends on the specific use and conditions. “Food grade” alone is not a complete technical specification.
A reliable choice starts with evidence. Review the adhesive’s technical data, intended-use documentation, and migration-related information for the exact laminate and process. Then check how it performs under real conditions: curing time, line speed, heat exposure, and contact with oils or moisture. Ask suppliers for test results tied to your structure, not just general claims. That sounds straightforward. It often isn’t. A laboratory result may not reflect a fast production line or a poorly controlled cure. The best selection is therefore a documented match between adhesive, packaging design, and actual use—not a label chosen in isolation.
Understand the Role of Food-Grade Laminating Adhesives
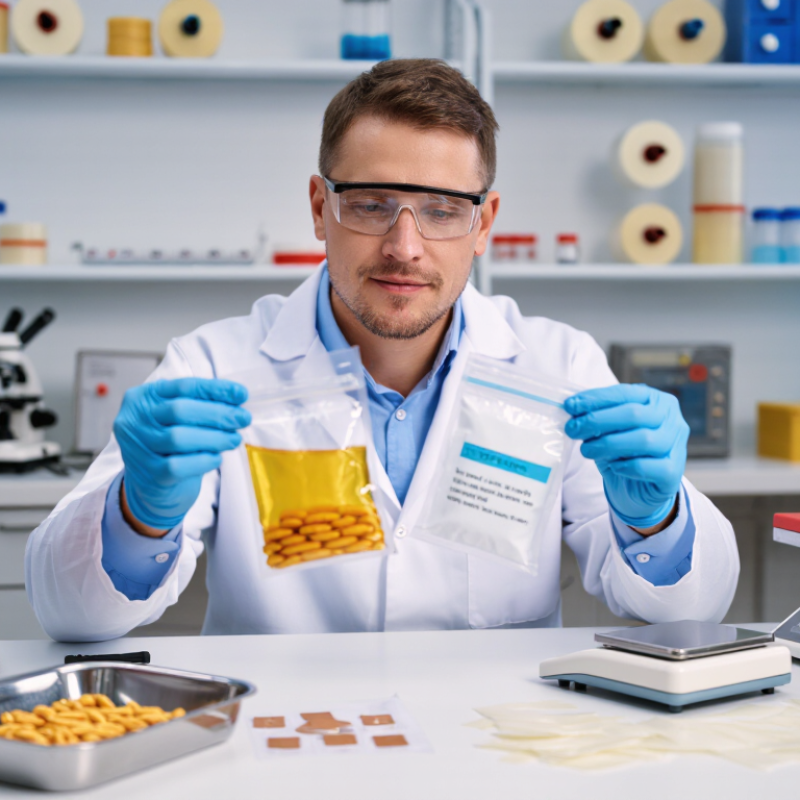
A laminating adhesive does more than hold two films together. It helps a package resist splitting, keeps oxygen and moisture barriers aligned, and protects the seal during filling and transport. In a chilled-food pouch, that bond may face condensation, pressure, and repeated handling. Small defects matter. The Flexible Packaging Association’s 2023 State of the U.S. Flexible Packaging Industry valued the sector at $42.9 billion in 2022 and identified food as its largest end-use market. That scale makes adhesive performance a practical food-packaging concern, not a minor material detail.
“Food-grade” is not a magic label. An adhesive suitable for one laminate, food type, or processing temperature may not suit another. Check intended use, curing conditions, bond strength, and migration data for the complete structure—not just the adhesive in isolation. For a retort pouch, for example, test the finished laminate after heat exposure; a bond that looks sound before processing may weaken later. Ask for technical documentation and independent test results, then confirm them against your actual packaging conditions. One caveat: test data cannot predict every production variation, so line trials still matter. The overlooked detail is often the simplest: allow the adhesive to cure fully before filling.
How to Choose Food Grade Laminating Adhesive? - Understand the Role of Food-Grade Laminating Adhesives
| Selection Dimension | What to Check | Why It Matters | Practical Selection Guidance |
|---|---|---|---|
| Food-contact compliance | Applicable regulations, intended market, adhesive formulation, and supplier documentation. | Suitability depends on the complete packaging construction and conditions of use; an adhesive is not food-safe simply because it is used in food packaging. | Confirm compliance for the specific structure, food type, contact conditions, and destination market. In the EU, assess relevant framework and good-manufacturing-practice requirements; plastic-layer rules do not automatically authorize every adhesive. |
| Food-contact arrangement | Whether the adhesive is behind a functional barrier or could contact food directly. | Direct contact and potential transfer through packaging layers can affect migration assessment and material suitability. | Provide the supplier with the full layer sequence, layer thicknesses, seal areas, and intended use. Obtain an assessment for the finished packaging construction. |
| Adhesive chemistry | Whether the system is solvent-based, solvent-free, or water-based, and whether it is one-component or two-component. | Different systems have different processing, drying, curing, and residual-solvent considerations. | Choose a system compatible with the substrates and converting equipment. Review technical and safety documentation, and confirm any required mixing or drying controls. |
| Substrate compatibility | Film or foil types, surface treatment, coatings, ink coverage, and bond between each layer. | Low surface energy, ink, coatings, or contamination can reduce wetting and adhesion. | Test the actual printed and unprinted materials, including the intended treatment level and surface condition. Do not rely solely on results from a different film grade. |
| Intended food and use conditions | Food composition, storage duration, temperature, and whether the pack is refrigerated, frozen, heated, or used for retort processing. | Oil, moisture, heat, and long storage can affect packaging performance and the conditions used for compliance assessment. | Match the adhesive and test plan to the most demanding intended use. Confirm suitability for hot filling, pasteurization, sterilization, or microwave use only where applicable. |
| Bond performance | Peel strength, bond uniformity, resistance to delamination, and performance after conditioning. | Reliable bonding helps maintain package integrity during converting, filling, transport, and storage. | Set acceptance criteria with the packaging converter and test samples after the specified cure and relevant temperature or humidity conditioning. |
| Cure and line conditions | Coating weight, mixing ratio where applicable, drying, laminating speed, nip conditions, and cure time. | Incorrect processing can lead to incomplete cure, weak bonds, or unacceptable residuals. | Follow the supplier’s current technical instructions and validate the production window on the intended equipment before routine manufacture. |
| Migration and sensory assessment | Overall and specific migration where applicable, potential transfer through layers, and odor or taste impact. | Packaging components can transfer substances or affect food sensory quality under certain conditions. | Use a qualified assessment based on the finished structure and intended conditions. Include sensory checks where odor or flavor neutrality is important. |
| Quality and traceability | Batch identification, change control, certificates or declarations, and supporting test information. | Documented controls help maintain consistent packaging performance and support audits or investigations. | Keep current technical and compliance documents, record adhesive batches, and reassess the construction after changes to formulation, substrates, inks, or process. |
Important: “Food grade” is not a universal approval. Verify compliance for the complete packaging structure, its intended food contact, and the applicable market requirements.