2026 Best Powder Feeder Buying Guide for Global Buyers
Choosing the right Powder Feeder can shape production accuracy, uptime, and product quality. For global buyers, the decision involves more than comparing prices or motor ratings. Material behavior matters. Fine powders may bridge, absorb moisture, or form uneven flow. Granules can behave differently from cohesive pharmaceutical excipients or food ingredients. A feeder that performs well in a laboratory may struggle beside a vibrating conveyor or high-speed packaging line.
This 2026 buying guide examines practical factors for international procurement. It covers feed-rate accuracy, hopper design, screw selection, control systems, cleaning access, and equipment compatibility. It also considers documentation, electrical requirements, language support, spare parts, and after-sales service. These details often decide whether installation remains smooth after delivery. Experienced engineers usually request material tests, sample runs, and operating data before approving a purchase. Reliable suppliers should explain tolerances clearly and provide traceable test records. Certifications must match the destination market and the intended, lawful application.
Real installations are rarely perfect. Dust levels change. Operators make adjustments. A small change in moisture can affect flow. Buyers should question optimistic claims and measure performance under realistic conditions. No guide can remove every uncertainty. However, careful specifications and transparent supplier communication can reduce expensive mistakes. The following sections help distributors, manufacturers, and engineering teams compare Powder Feeder options with greater confidence, technical discipline, and long-term value.
Powder Feeder Fundamentals and Core Functions
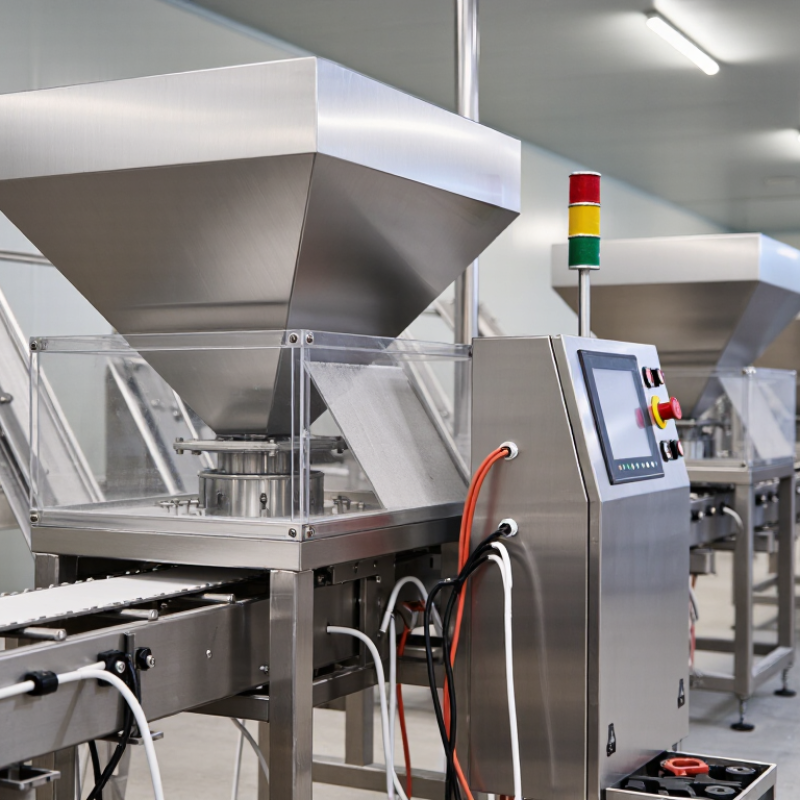
A powder feeder is a controlled dosing device that moves dry material from a hopper into a process line or container. Its main components include a hopper, agitator, feeding screw or rotary disc, drive system, and control panel. Each part affects consistency. Fine powders may bridge above the outlet. Damp powders can cake around the screw. Granular powders may separate during vibration.
The feeder’s core function is maintaining a predictable feed rate. Volumetric models rely on fixed volume, while gravimetric models measure weight continuously. Gravimetric control usually offers better accuracy when bulk density changes. However, it needs correct calibration and stable load-cell installation. A small airflow error can disturb readings. Clean, steady airflow matters.
Practical testing should examine startup, shutdown, refill behavior, and low-level hopper operation. Check whether the feeder delivers smoothly at both minimum and maximum rates. An agitator may improve flow, but excessive movement can damage fragile particles or increase dust. This detail is easy to overlook. Buyers should also review contact materials, cleaning access, electrical compatibility, noise, and available technical documents. No feeder suits every powder. Product trials remain necessary, and even experienced engineers sometimes revise the initial selection after observing real material behavior.
2026 Best Powder Feeder Buying Guide for Global Buyers
Powder Feeder Fundamentals and Core Functions
Feed-rate requirements vary with production scale, powder bulk density, flowability, and the required dosing accuracy. The ranges below are generalized engineering planning values for common powder-feeding applications; actual specifications should be confirmed through material testing and feeder trials.
Core functions to evaluate include stable mass flow, repeatable dosing, hopper bridging prevention, refill control, easy cleaning, and compatibility with fine, cohesive, or abrasive powders.
Main Powder Feeder Types and Their Operating Principles
Powder feeders regulate dry materials into mixers, reactors, fillers, and packaging lines. Their performance depends on powder flow, moisture, particle size, and bulk density. In 2026, buyers should study operating principles before comparing capacity or price. Real installations often reveal differences that brochures do not mention.
Volumetric feeders deliver powder by measuring a fixed screw volume or cavity rotation. They are simple and affordable, but output changes when density shifts. Gravimetric feeders weigh material continuously and adjust speed automatically. This principle offers better accuracy during batch changes, although load cells need stable mounting and regular calibration. Loss-in-weight feeders use the same weighing concept while monitoring hopper weight decline. They suit precise dosing and long production runs. Not always easy.
Vibratory feeders move powder through controlled vibration. They work well with free-flowing materials but may struggle with cohesive or damp powder. Screw feeders provide stronger control and handle many industrial powders, yet bridging can occur above the screw.
Testing should include startup, refill, low-level operation, and cleaning. In plant trials, a feeder may perform accurately for ten minutes, then drift after humidity changes. That detail matters.
Buyers should request test data using their actual powder, not a similar substitute. A practical review also checks contact materials, dust sealing, inspection access, and control response. No feeder is perfect. A small design compromise can become a daily maintenance problem.
Key Specifications for Comparing Powder Feeder Performance
For global buyers, powder feeder performance starts with measurable specifications, not attractive brochures. Compare rated throughput, gravimetric accuracy, turndown ratio, and response time under real material conditions. A 2024 powder-handling equipment market report forecasts continued annual growth above 6%, reflecting stronger demand for controlled dosing and automation. That growth does not guarantee suitable equipment.
Material testing is essential. Record bulk density, moisture, particle size, cohesion, and angle of repose. ASTM D6393 supports standardized bulk-solids flow testing, while USP <1174> highlights flow behavior as a critical powder characteristic. For cohesive powders, a feeder may bridge inside the hopper or produce uneven discharge. Test both minimum and maximum rates. Short trials can mislead.
Control performance deserves equal attention. Check load-cell resolution, refill disturbance, calibration drift, and data logging. For hygienic applications, inspect tool-free access, dead zones, sealing, and cleaning time. The 2024 industry outlook from Powder & Bulk Solids identifies dust management and process reliability as recurring investment priorities. I would request at least eight hours of continuous testing, including start-up and refill cycles. Perfect accuracy on a dry test day means little in humid storage. This remains a judgment call. Suppliers should disclose test conditions, not only their best accuracy figure.
2026 Best Powder Feeder Buying Guide for Global Buyers - Key Specifications for Comparing Powder Feeder Performance
Use this comparison as a preliminary selection guide. Actual performance depends on powder flowability, cohesion, moisture, particle-size distribution, bulk-density variation, feeder configuration, calibration method, and installation conditions.
| Feeder Technology | Typical Throughput Range | Typical Metering Accuracy | Suitable Powder Characteristics | Typical Particle Size | Bulk-Density Handling | Common Hopper Capacity | Main Advantages | Key Limitations and Buying Checks |
|---|---|---|---|---|---|---|---|---|
| Loss-in-Weight Screw Feeder | Approximately 0.1–2,000 kg/h, depending on screw diameter, pitch, and material | Typically ±0.25% to ±1.0% of setpoint after calibration | Free-flowing, cohesive, dusty, and mildly difficult powders; twin-screw designs handle more cohesive materials | Commonly 1 μm–10 mm; verify screw clearance for larger particles | Usually suitable for bulk densities of about 0.1–2.0 kg/L, with calibration for density changes | Approximately 5–500 L | Continuous gravimetric control; automatically compensates for changes in bulk density and refill level | Higher cost and control complexity; check load-cell resolution, refill interruption, screw wear, dust sealing, and minimum stable feed rate |
| Volumetric Screw Feeder | Approximately 0.05–1,500 kg/h, depending on screw geometry and speed | Typically ±1% to ±5% of setpoint, assuming stable bulk density | Free-flowing and moderately cohesive powders with consistent bulk density | Commonly 10 μm–10 mm | Performs best when bulk density and powder aeration remain consistent | Approximately 2–300 L | Simple construction, lower initial cost, easy speed-based control, and compact installation | Output changes when density, moisture, or powder level changes; requires regular calibration and stable hopper conditions |
| Vibratory Feeder | Approximately 0.1–500 kg/h, depending on tray size and powder flowability | Typically ±1% to ±5% of setpoint for free-flowing materials | Dry, free-flowing granules, crystals, pellets, and powders with low cohesion | Commonly 50 μm–10 mm; very fine powders may bridge or fluidize | Best with stable-density materials; performance can decline with highly compressible powders | Approximately 1–100 L | Gentle handling, few moving parts, low shear, and convenient cleaning | Sensitive to powder cohesion, moisture, vibration transmission, and installation rigidity; not ideal for very fine dusty powders |
| Rotary Airlock Feeder | Approximately 0.5–20,000 kg/h, depending on rotor volume and speed | Typically ±2% to ±10% of setpoint; generally used for transfer rather than precision dosing | Dry powders, granules, and dust-collection materials requiring controlled discharge | Commonly 10 μm–15 mm; avoid particles that can damage rotor or housing clearances | Handles a broad density range, but capacity is strongly affected by fill efficiency and leakage | Usually integrated below a hopper, cyclone, or filter; upstream vessel volume varies widely | High capacity, continuous operation, and useful pressure separation between process zones | Not normally the first choice for high-accuracy dosing; check rotor clearance, abrasive wear, air leakage, explosion protection, and product temperature |
| Disc or Rotary-Cup Feeder | Approximately 0.05–200 kg/h, depending on disc speed and cavity volume | Typically ±1% to ±3% after calibration with consistent material | Free-flowing powders, granules, and small particles with relatively stable density | Commonly 50 μm–5 mm | Requires consistent filling of the disc or cups; density variation can affect mass output | Approximately 1–50 L | Accurate intermittent or continuous dosing, clear operating principle, and relatively gentle product handling | Bridging and inconsistent cavity filling can reduce accuracy; check cleanability, cavity size, and maximum allowable particle size |
| Loss-in-Weight Vibratory Feeder | Approximately 0.1–300 kg/h, depending on tray design and material properties | Typically ±0.5% to ±2% of setpoint after calibration | Free-flowing powders and granules where low shear and low mechanical contact are important | Commonly 50 μm–10 mm | Suitable for stable-density materials; gravimetric control helps correct for gradual density changes | Approximately 5–150 L | Combines gravimetric monitoring with gentle conveying and relatively simple product-contact geometry | Very cohesive or highly aerated powders may require agitation, vibration isolation, or an alternative screw-based design |
| Pneumatic Powder Dosing System | Approximately 0.1–5,000 kg/h, depending on conveying distance, air rate, and dosing device | Typically ±1% to ±5% for controlled dosing; conveying-only systems may be less precise | Dry powders and granules compatible with pneumatic conveying | Commonly 1 μm–10 mm; assess friability, electrostatic behavior, and conveying velocity | Can handle wide density ranges, but air entrainment changes apparent flow behavior | Approximately 5–1,000 L, depending on the pressure or vacuum vessel | Flexible routing, enclosed transfer, long-distance conveying, and reduced mechanical contact | Requires compressed air or vacuum; check filtration, moisture control, wear, dust explosion protection, and product degradation |
Buyer checklist: Compare the guaranteed minimum and maximum feed rates, accuracy basis, calibration procedure, turndown ratio, refill method, dust-tightness, contact-material compatibility, cleaning time, power and air requirements, control-system interface, safety certification, spare-parts availability, and performance-test conditions.
How to Select a Powder Feeder for Global Applications
2026 Best Powder Feeder Buying Guide for Global Buyers
How to Select a Powder Feeder for Global Applications
Selecting a powder feeder starts with the material, not the machine catalog. Record particle size, moisture, bulk density, flowability, and expected feed rate. A cohesive powder may bridge inside a narrow hopper. A free-flowing powder can flood the process. These differences affect screw design, agitation, and control accuracy.
For global applications, check whether the feeder supports local voltage, language settings, and available spare parts. Request calibration data across the full operating range, not only at one target rate. Loss-in-weight systems often provide strong accuracy, but vibration and refill changes can disturb readings. Gravimetric control is useful when density varies. Volumetric feeding may suit stable powders with simpler production needs.
Tips
Run a practical material trial before purchase. Use your actual powder and container geometry. Measure start-up behavior, refill recovery, cleaning time, and dust control. Confirm contact materials, surface finish, and documentation for your industry and destination market. Ask about remote support and technician training. Small details matter.
I once underestimated humidity during a feeder evaluation. The powder looked stable in the laboratory, then formed soft lumps during a longer test. That experience changed my checklist. Environmental testing is not optional for cross-border projects. Still, no feeder solves every handling problem. Review the process around it, and challenge optimistic test results.
Installation, Calibration, Maintenance, and Safety Requirements
Install the powder feeder on a rigid, level frame with enough space for inspection. Check local voltage, grounding, and enclosure requirements before connecting power. Keep the hopper away from vibration, heat, and direct airflow. A short, clean transfer tube reduces powder buildup. Use guards around moving parts, and apply lockout procedures before adjustments. Dust extraction may be necessary when handling fine powders.
Calibration should match the actual material, not only the factory setting. Tare the container, run a measured batch, and compare the output with a certified scale. Repeat the test at low, medium, and high feed rates. Record humidity, powder temperature, screw speed, and batch weight. Small changes can reveal bridging or inconsistent flow. Calibration may look stable today and fail tomorrow, so recheck after material changes.
Inspect seals, screws, and tube connections each shift. Remove residue with approved tools; avoid compressed air if it spreads dust. Check emergency stops and protective covers weekly. Keep a maintenance log with dates, readings, and corrective actions. Do not guess when powder behaves strangely. Stop the feeder, isolate energy, and investigate the cause. Some powders absorb moisture quickly, so open containers should not remain beside the feeder. Local safety rules and professional risk assessments still apply.
English
Česká republika
Deutsch
Dutch
Polska